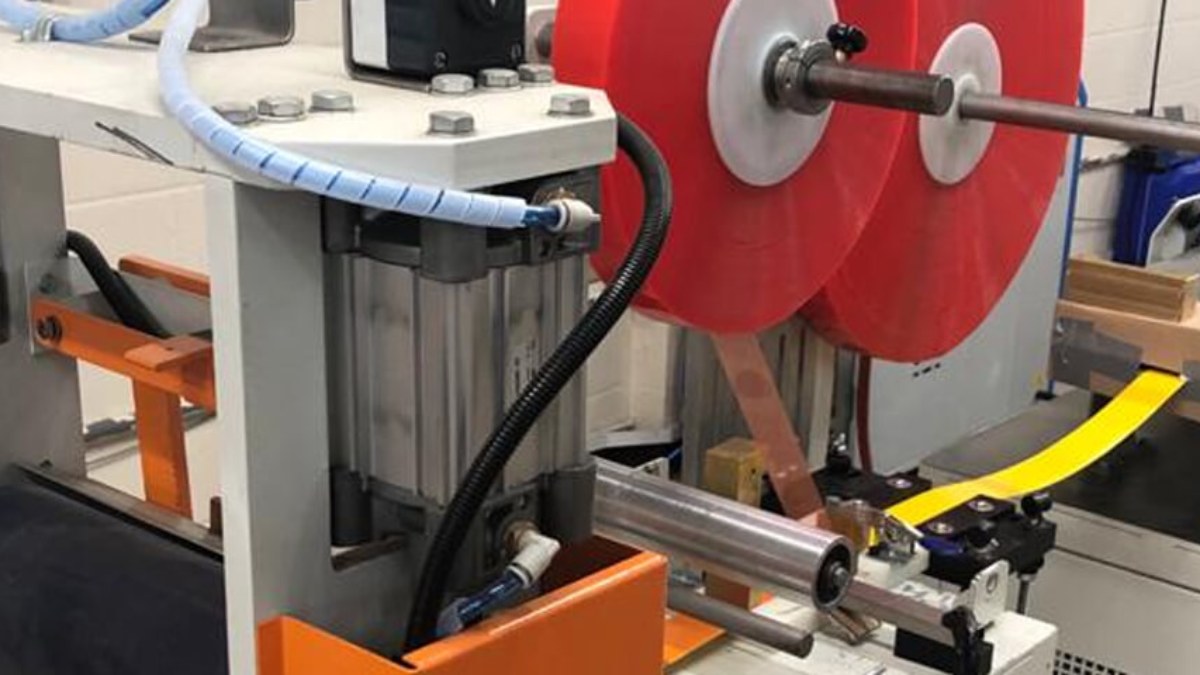
Most floor marking fails in the same way. The colour wears thin where the forklifts turn, the edges lift, and within a year the line that was supposed to keep pedestrians away from moving plant is a grey smudge. That failure almost always traces back to how the product was made rather than how it was fitted. This month we are looking at the machine that sits at the heart of our floor marking output: the PermaStripe extruder. If you specify or buy line marking for a working warehouse, understanding what happens on that machine tells you a great deal about what you can expect from the tape on your floor.
Why the construction of a floor marking tape decides its lifespan
There are broadly two ways to make a coloured marking tape. The cheap route is to take a clear or neutral carrier film and print or laminate the colour onto the surface. It looks identical to the alternative on day one. The problem is that all of the colour lives in a layer a few microns thick, so the first pass of a pallet truck wheel that scuffs the surface takes the colour with it.
The other route is extrusion, where the pigment is mixed into the polymer before the material is ever formed into a film. The result is a homogeneous product: cut through it at any point and the colour runs all the way from the top surface to the adhesive. Scratches and scuffs still happen, but they do not expose a different colour underneath, so the line stays legible. That is the principle behind our PermaStripe floor marking tape, and it is the reason we run our own extrusion line rather than buying in printed film.
What the PermaStripe extruder actually does
The machine is best thought of as a series of controlled stages rather than a single process. Each one affects a property that matters to the end user.
Compounding and colour
The process starts with raw PVC, plasticisers, stabilisers and pigment being blended into a compound. Getting this stage right governs two things: the shade of the finished tape and how flexible it is. Too rigid and the tape will not conform to the small undulations in a concrete floor; too soft and it deforms under sustained point loads. Because we mix in-house, colour is controlled against a reference rather than accepted from a supplier’s batch, which is what allows consistent yellow across orders placed months apart.
Melting, the die and thickness control
The compound is fed into the extruder barrel, where a heated screw melts and homogenises it. The molten material is then forced through a wide flat die to form a continuous sheet, which passes through calibrating rollers that set the final gauge. Thickness matters more than people expect. A marking tape needs enough body to survive abrasion and to take a bevelled edge, but a thick, hard-edged product becomes a trip hazard and a snag point for pallet truck wheels. The roller gap is where that balance is set, and it is monitored continuously across the web width so the tape is not thicker on one edge than the other.
Surface finish, including PermaStripe Smooth
While the sheet is still hot it passes an embossing roller, and this is where the different finishes in the range are created. The standard product carries a subtle textured finish that helps with slip resistance and hides scuffing. Where a cleanroom, food production area or retail environment needs a surface that can be wiped or scrubbed without dirt collecting in the texture, PermaStripe Smooth is produced by running the same compound through a polished roller instead. The core construction and performance are unchanged; only the top surface differs. That is worth knowing when you are specifying, because it means you are not trading durability for cleanability.
After cooling, the web is trimmed, coated with adhesive and liner, then slit to width and wound. Slitting in-house is what makes non-standard widths practical without a long lead time.
What in-house extrusion means for you as a buyer
Owning the machine changes what we can offer beyond the product itself:
- Batch-to-batch consistency. A repeat order should match the lines already on your floor, not sit a shade off.
- Custom colours. Because pigment is added at the compounding stage, specific Pantone or RAL references can be produced to order, subject to a minimum quantity.
- Control of lead times. Production is scheduled here rather than queued behind another company’s priorities.
- Traceability. If a question arises about a particular roll, it can be traced back to a production run.
The wider extruded range
The same core process supports several products aimed at different problems. PermaLean homogeneous marking tape covers 5S and lean manufacturing layouts, with six standard colours plus hazard patterns for kanban zones, tool shadowing and equipment footprints. For sites where marked routes need to remain visible during a power failure or smoke event, PermaRoute photoluminescent floor marking combines a glow finish with ESD-safe performance.
Practical takeaway
When you are comparing floor marking quotes, ask one question: is the colour extruded through the product or applied to the surface? Everything else — installation time, repaint cycles, the state of your gangway markings in two years — follows from the answer. The extruder is not glamorous machinery, but it is the reason a peel-and-stick line can outlast painted marking in a busy distribution centre without solvents, curing time or floor downtime.
If you are planning a layout change or a marking refresh and are unsure which finish suits the floor and the traffic, our technical team can advise on the right specification before you order.